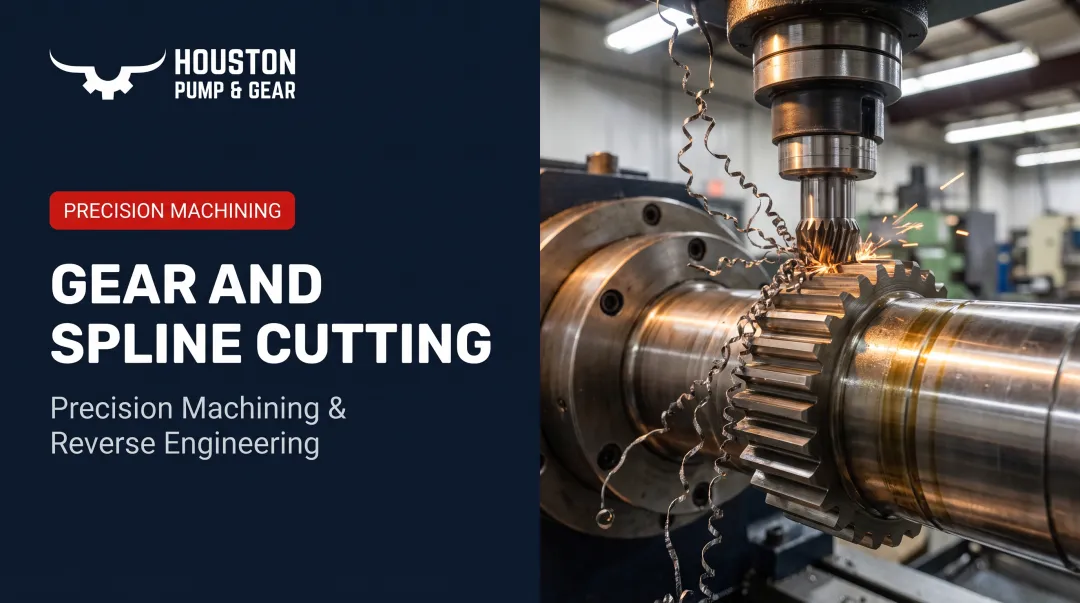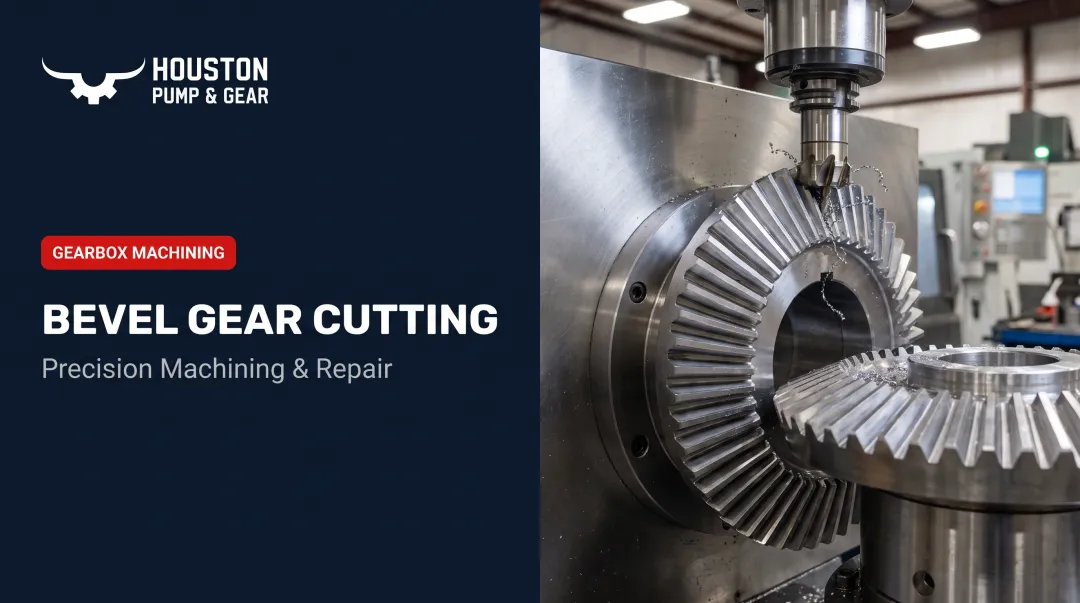

Gear broaching is the machining process behind the internal splines, keyways, and precision gear forms that keep couplings aligned and load properly transferred inside industrial gearboxes. This guide breaks down what broaching is, how the process actually works, how it compares to hobbing, and when you need a specialized repair shop instead of a general machinist.
Key Takeaways
- Broaching finishes a spline or keyway profile in one pass with a progressively toothed tool
- Internal splines and keyways in gearbox bores and couplings are cut most efficiently by broaching
- Hobbing generates external gear teeth by rotation; broaching cuts internal forms in one linear stroke
- Broaching-capable machining on call can cut power plant outages from weeks to days
What Is Gear Broaching?
Broaching is a machining process where a specialized toothed tool, called a broach, is pulled or pushed through a workpiece to remove material in a single controlled pass. Unlike drilling or milling, which require multiple operations to rough and finish a shape, a broach does the entire job in one stroke.
The purpose is straightforward: produce splines, keyways, and gear tooth forms with tight tolerances and excellent repeatability, without the setup changes that slow down other methods. Each tooth on the broach is cut slightly larger or shaped differently than the one before it, so the tool builds the final profile as it travels through the material.
Materials that broach well include steel alloys, aluminum, brass, and bronze. Hardness matters too. Gear Technology cites an ideal working range around HB 200-230 (roughly HRC 14-21), with materials up to about HB 300 (HRC 32) commonly broached without trouble. Harder material isn't impossible, but it changes tool wear and cycle planning.
How the Tooth Design Works
A typical broach has three functional zones:
- Roughing teeth — remove the bulk of the material in incremental steps
- Semi-finishing teeth — refine the shape closer to final dimensions
- Finishing teeth — equal-size teeth that set the final geometry and surface finish
This progressive design means a pilot hole can become a finished involute spline or keyway in one pull of the tool, according to Gear Technology's broaching fundamentals overview. No re-chucking, no tool changes mid-cut.
Internal vs. External Broaching
- Internal broaching cuts splines, keyways, and other forms inside a bore. It needs a pre-drilled or pre-bored pilot hole and a fixture that keeps the workpiece from shifting during the cut.
- External (or pot) broaching works the opposite way — the part is pushed or pulled through a stationary tool to cut features on its outside diameter.
Most gearbox repair work involving worn couplings or shafts falls into the internal category, since that's where splines and keyways typically live.
The Gear Broaching Process Step by Step
Broaching a spline or keyway follows a consistent sequence, whether it's a new part or a repair job.
- Prepare the workpiece. For internal work, this means pre-drilling or pre-boring the pilot hole, chamfering the edge, and securing the part in a fixture that resists movement during the cut.
- Select and set up the tool. The shop chooses a broach with the correct roughing, semi-finishing, and finishing geometry for the required spline or tooth form. Wrong broach geometry produces the wrong profile.
- Run the cutting pass. The broaching machine's elevator and puller mechanism draws (or pushes) the tool through the material. Cutting fluid cools the tool, lubricates the cut, and clears chips as they form.
- Remove and inspect the part. Technicians check dimensional accuracy, tooth or spline profile, and surface finish against tolerance requirements before the part moves on.
- Maintain the tooling. Broaches need periodic resharpening and eventual replacement to keep cutting consistent across a production or repair run.

One documented electromechanical pot-broaching system achieved cycle times of 12-30 seconds per part, with cutting speeds up to 9.13 m/min (about 30 ft/min), according to Gear Solutions. That figure applies to that specific machine, not every job. A large gearbox spline repair with custom tooling will run longer, but shops still turn to broaching when they need both speed and consistent profiles.
Broaching vs. Gear Hobbing: What's the Difference?
Hobbing and broaching solve different problems, even though both cut gear-related forms.
Gear hobbing is a rotary generating process. A hob and the workpiece rotate in sync while the hob is fed across the blank, gradually cutting external gear teeth over multiple rotations. It's the standard method for spur, helical, and worm gears.
Broaching cuts in a single linear stroke, and it's built for internal geometry: splines, keyways, and other bore-side features that hobbing simply can't reach.
| Factor | Broaching | Hobbing |
|---|---|---|
| Geometry produced | Internal splines, keyways, forms | External cylindrical gear teeth |
| Motion | Single linear pull/push stroke | Continuous rotary generation |
| Best fit | High-precision internal repeatability | Spur, helical, worm gears |
| Volume strength | Strong once tooling is cut | Flexible across high and low volume |
Broaching's controlled cutting action tends to reduce vibration and can deliver tighter tolerances than hobbing. Neither process has a single universal tolerance figure that applies across every job. Actual results depend heavily on part size, material, and tooling condition.
Gear shaping uses a reciprocating cutter that meshes with the workpiece. It can reach internal gears, blind-ended forms, and teeth near shoulders where neither broaching nor hobbing works cleanly.
Given a damaged part, an experienced machine shop won't default to one method. They'll look at bore access, whether the geometry is blind or through, available tooling, required fit, and lot size before recommending broaching, hobbing, or shaping.
Types of Broaches and Broaching Machines
Broaching tooling and machines vary by gear geometry, bore or blank size, and production volume.
Linear vs. rotary broaching:
- Linear broaches move in a straight line through or across the workpiece
- Rotary broaches spin at a slight offset angle, creating a wobbling cut ideal for hex, square, and other polygon forms
Push vs. pull:
- Pull broaches are common for internal work, drawn through a pre-bored hole
- Push broaches suit shorter cuts such as keyway slotting
Horizontal vs. vertical machines:
- Horizontal machines fit low quantities, frequent tool changes, or shops with limited ceiling height
- Vertical machines suit higher quantities, tighter tolerances, and limited floor space
Common broach types in gear work:
- Keyway broaches — cut internal keyway slots
- Spline broaches — generate spline profiles inside a bore
- Pot broaches — cut external gear teeth or splines on cylindrical parts
- Helical broaches — produce helical internal or external forms

The right combination depends on part size, precision requirements, and whether it's a one-off repair or a production run.
Applications in Power Plants and Heavy Industry
Precision internal splines and keyways aren't a niche concern. They're load-bearing connections that keep critical industrial equipment running.
Involute splines transmit high torque by sharing the load across multiple teeth simultaneously, giving them more capacity than a single keyway connection. But that only works if the geometry is accurate.
Pitch deviations and misalignment cut the number of teeth actually sharing the load. Stress shifts toward tooth edges and raises fatigue risk over time. Re-machining a worn spline to spec, rather than living with a degraded fit, protects the coupling long-term.
Houston Pump & Gear handles this work for power plants and heavy industry across Texas and Louisiana. In-house CNC machining centers, boring mills, and turning centers support precision internal machining.
The shop's 24/7 emergency response has been tested under real pressure. When a Lufkin S2212C gearbox sent a power plant into an emergency shutdown, a truck was dispatched the same day, and the unit was back in service within 72 hours. That customer has since had more than 15 units serviced.
Industries relying on this level of precision include:
- Power generation
- Oil and gas
- Mining
- Chemical and petrochemical processing
- Steel and heavy manufacturing
When a coupling is out of alignment or a spline shows wear, the fix usually comes down to two paths: repair the existing bore feature, or replace the unit. Houston Pump & Gear's refurbished gearbox exchange ratio-matches and spin-tests replacement units under a 12-month warranty.
Frequently Asked Questions
What is the purpose of broaching?
Broaching creates precise, repeatable internal splines, keyways, and gear tooth forms in a single machine pass. It's valued for tight tolerances and consistency across repair or production runs without multiple setups.
What is the difference between broaching and hobbing?
Broaching cuts internal forms like splines and keyways in one linear stroke. Hobbing rotates a hob and workpiece together to generate external gear teeth gradually. They target different geometries entirely.
What is the broaching process step by step?
- Prepare a pilot hole and secure the part in a fixture.
- Pull the toothed broach through the material while coolant clears chips.
- Inspect the part against tolerance and finish requirements.
What materials can be broached?
Steel alloys, aluminum, brass, and bronze all broach well. Materials up to roughly HB 300 (HRC 32) are commonly handled, though harder materials require adjusted tooling and cycle planning.
Can a damaged gearbox spline or keyway be repaired through broaching?
Yes. Re-machining or re-broaching can often restore a worn internal spline or keyway to spec if the housing and related components are still sound. When damage is severe or parts are missing, a refurbished exchange unit is often the faster path back to production.
How long does a gear broaching repair take?
Turnaround depends on part complexity, tooling availability, and whether replacement components are needed. Typical custom machining repairs fall in the 1–2 week range. Emergency response can move much faster, including a documented 72-hour gearbox turnaround for a power plant client.